A spiral freezer belt inspection before shipment should check six things: edge welds finished flush, no arc burns or grinding marks at the joints, straight rods, pitch and edge links in line along the roll, a clean belt with no oil or particles, and an even surface after pickling. Ask your supplier for photos and readings of each.
A spiral freezer belt runs for thousands of hours in the cold, under tension, around a drum. Most problems that stop a spiral line early — a weld that cracks at the edge, a rod that is not straight, a belt that wanders on the drum — can be seen on the belt before it is packed. The question is whether anyone looks.
If you buy spiral freezer belts for your own equipment or as replacements, these are the six checks I ask our team to make on every roll, and what a pass and a reject look like. Our Spiral Freezer Belts are produced by qualified production partners to the drawing you approve; JBL Mesh Belt does the engineering review and the pre-shipment inspection.
What do the numbers look like on a real spiral belt project?
| Project | Check | Original belt | New belt |
|---|---|---|---|
| Bakery spiral cooling, Melbourne, Australia · 2023–2024 · about 400 m | Pitch | 27.41 mm | 27.40 mm |
| Rod diameter | 5.03 mm | 5.00 mm | |
| Link thickness | 2.70 mm | 2.70 mm | |
| Waffle cooling spiral · belt and sprockets replaced | Link thickness | 2.42 mm (worn) | 2.71 mm (new, wear corrected) |
| Rod | 4.99 mm | Matched to the original | |
| Spiral belt replacement, Malaysia · 2026 | Rod pitch, trial run vs bulk belt | 19.05 mm (trial) | 19.05 mm (bulk) |
| Turn | — | Full-circle turn test before packing |
Readings are from the named projects, taken with a caliper on the sample or belt. They show how a record is kept, not universal values. Full cases: Melbourne · waffle cooling spiral · Malaysia.
How should the edge welds on a spiral freezer belt look?
The edge carries the belt tension around the drum. A weld that stands proud of the link catches, wears and can crack under repeated load.
Weld position and finish against the approved drawing; a raised weld bump is rejected and reworked.
Inspection photos of the edge welds on your rolls. Where your project needs it, a weld-strength check on sample sections, with the method agreed before production.
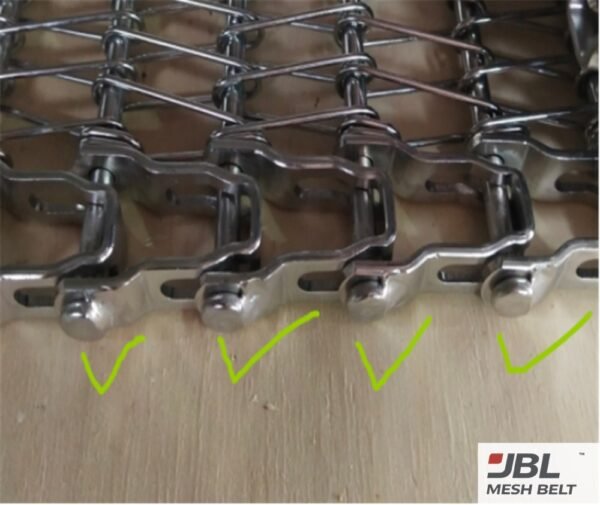 Accepted
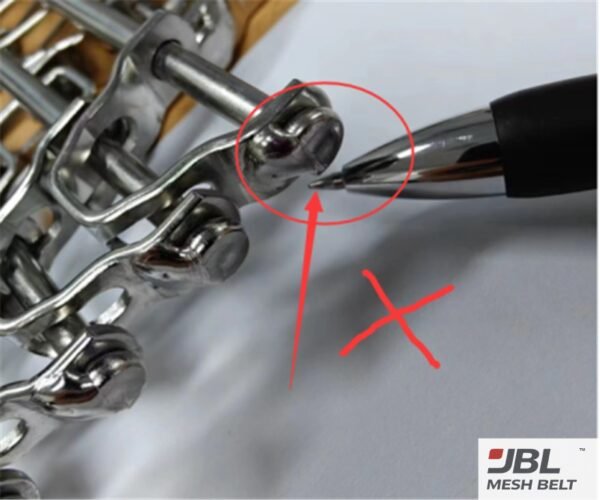 Rejected
Food lines: weld burrs are also a contamination risk. Read spiral freezer belt weld burrs and IQF contamination.
What marks around the joints should be rejected?
An arc burn or a heavy grinding mark at a rod joint weakens the area and leaves a rough surface where product and debris can catch.
Rod joints and centre-link welds are inspected for arc burns and grinding marks; affected sections are rejected.
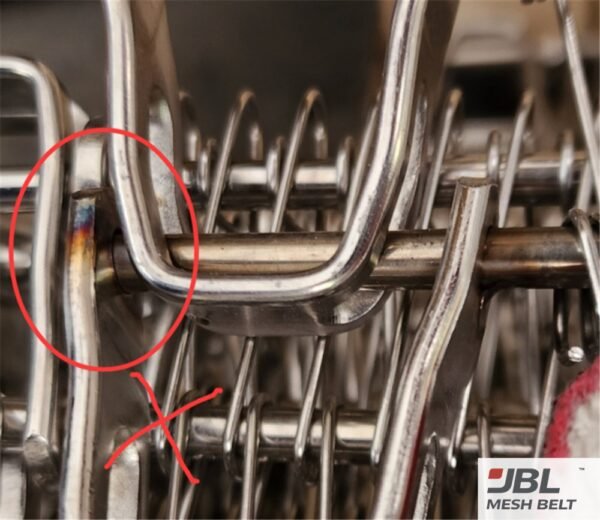 Rejected
Most problems that stop a spiral line early can be seen on the belt before it is packed.
Spring Liu, JBL Mesh Belt
Why does rod straightness matter on a spiral belt?
A bent rod lifts the mesh, changes how the belt sits on the drum and spreads uneven load to the links beside it.
Rods are checked for straightness on sample sections; rod and spiral wire fit follow the approved drawing.
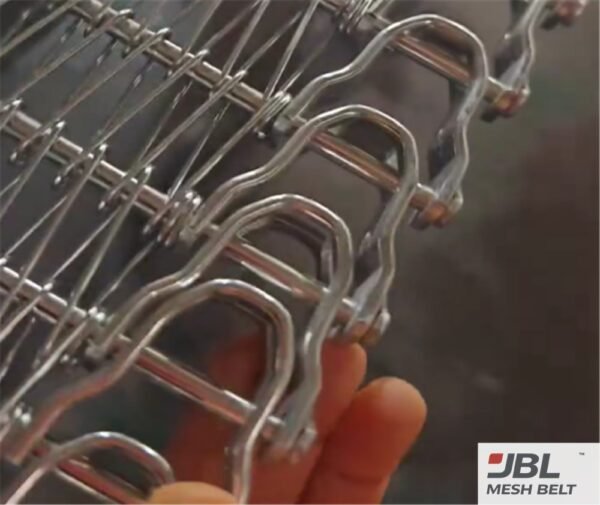 Check
How is pitch checked along the roll?
If pitch drifts or edge links are out of line, the belt engages the drive unevenly and starts to wander or climb.
Pitch is measured at several points along each roll and compared with the drawing; edge links and rods are checked for alignment.
The pitch readings for your rolls — like the 19.05 mm trial and bulk readings in the table above.
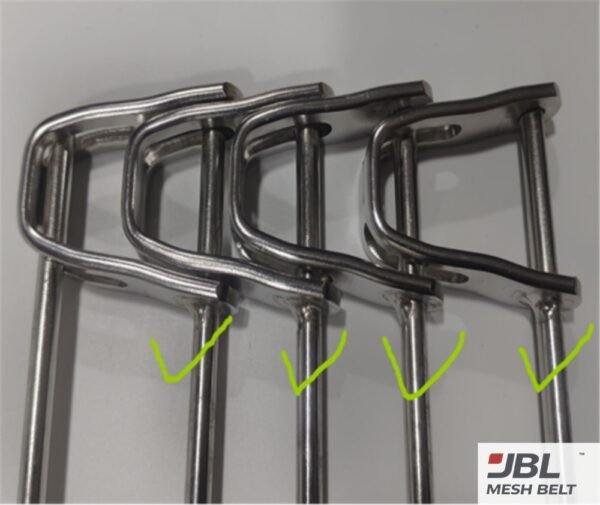 Accepted
What makes a new spiral belt clean enough to ship?
Oil residue or a loose particle on a new belt ends up in the product on the first run.
The mesh is inspected for oil residue and foreign particles before packing; a belt that fails is cleaned and rechecked.
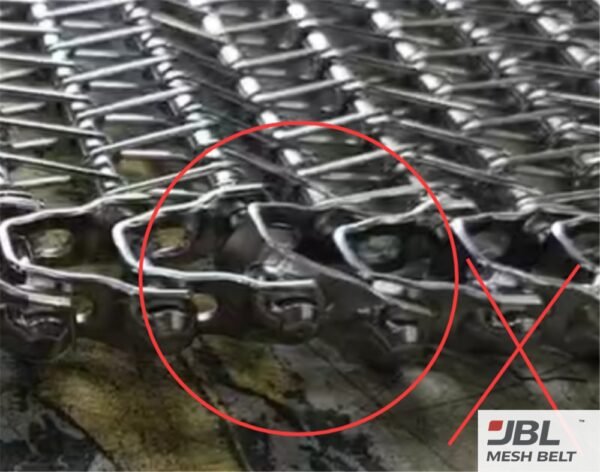 Rejected
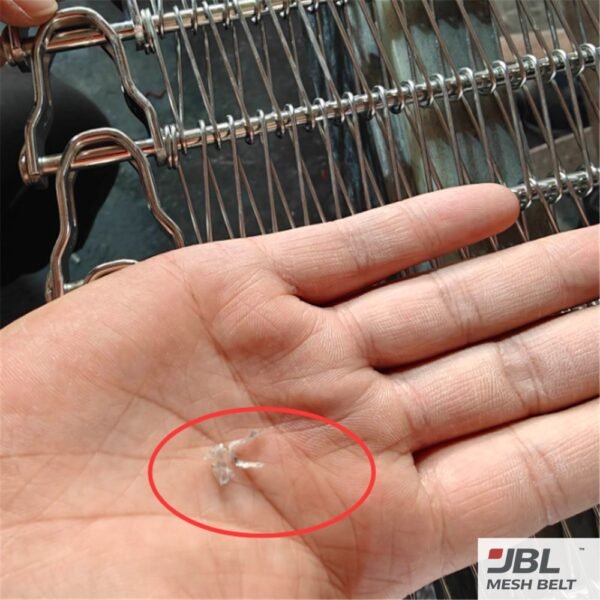 Rejected
What should the surface look like after pickling?
Stains or uneven colour after pickling can point to a surface that was not fully treated.
Surface colour and stains after pickling, section by section.
When is the turn ratio confirmed?
On paper, before production. The belt’s collapse around the drum has to match your spiral. We review it against your drum or cage at the drawing stage and confirm the value with you in writing — it follows your equipment, not a catalogue figure. In the Malaysia project the bulk belt was also laid out in a full circle before packing to check that the mesh closed evenly.
Further reading: spiral belt turn ratio, load, tracking and service life.
Replacing a spiral belt on an existing freezer?
Same width and pitch do not confirm a fit. Drive type, edge design, turn ratio and the condition of your sprockets all decide whether the new belt runs. In the waffle cooling project the original link read 2.42 mm after years of wear; the new link was made at 2.71 mm, so the wear was corrected, not copied. Send photos of the old belt’s edge and drive side, and your drum details.
See also: spiral freezer belt replacement compatibility guide.
Spiral freezer belt inspection: FAQ
Do you inspect every roll?
Yes. Every roll is checked against the approved drawing before packing, and the agreed records go to you before shipment.
Can I see the inspection before the belt ships?
Yes. You receive inspection photos and the agreed check results for your order before shipment.
Do you test weld strength?
Where your project calls for it, a weld-strength check on sample sections is agreed before production, with the method written down.
What turn ratio should my belt have?
It follows your drum or cage and the belt design. We confirm it with you in writing at the drawing stage rather than quote a standard value.
How do price and lead time work?
They depend on size, material and quantity and are confirmed in writing in each quotation.
Send a photo of your belt edge
A photo of the edge and drive side, or your drawing, is enough to start. Send your drawing or old-belt photos on WhatsApp. No sales calls.