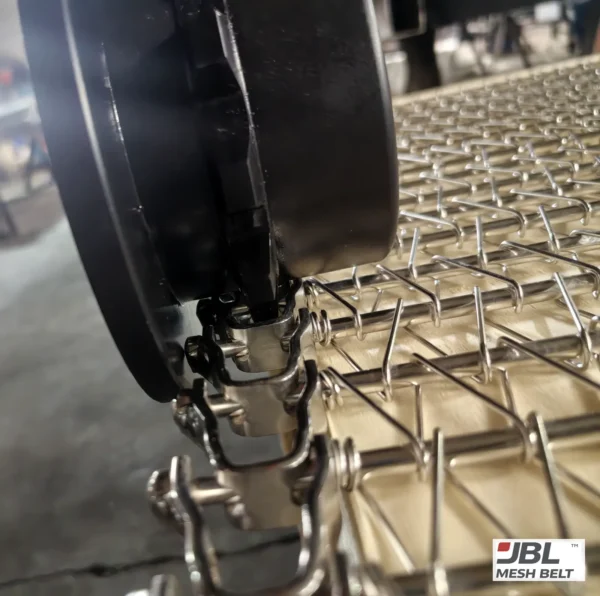
Drive engagement is decided at the design stage, not at installation. Before you release a new spiral conveyor design, check the belt pitch, the edge where the drive touches the belt, the turn ratio, and the sprocket tooth, bore and material together, as one system. Many engagement problems I see later started as a belt and a sprocket that were specified separately.
I work with OEMs and plant engineers on spiral freezer, cooling and self-stacking belts. When a project reaches me after the machine is built, the questions are about wear and jumping. When it reaches me before the drawing is released, the same problems can be designed out. This article is the checklist I use at that earlier stage.
What does “drive engagement” mean on a spiral conveyor belt?
Drive engagement is the point where the machine moves the belt. It is not the same on every spiral:
| Drive arrangement | Where the drive meets the belt | What has to match |
|---|---|---|
| Low-tension (friction) drum | The drum bars against the belt’s inner edge | Inner edge, link collapse, turn ratio, weld finish |
| Direct drive at the drum | The drum engages the inner edge positively | Edge geometry and pitch, kept in step with the drum |
| Side drive | Sprockets on the side links | Rod pitch and tooth, plus turn ratio on the drum |
| Edge drive | Sprockets on roller chains at both edges | Chain model and pitch, rod pitch as a multiple of chain pitch |
| Drive and take-up sprockets (many spirals) | Teeth on the rods or links outside the drum | Pitch, tooth profile, tooth count, bore and alignment |
In each case, the belt and the part that drives it must be designed to the same numbers. A belt drawing and a sprocket drawing made by two people at two times is where mismatches start. For a deeper look at the drive types themselves, see how your freezer’s drive changes the belt you need.
Which belt dimensions decide engagement?
Pitch is the obvious one. It is not the only one.
| Belt dimension | Why it matters for engagement | What I ask for on the drawing |
|---|---|---|
| Rod pitch / link pitch | The tooth or drum must meet the belt at the same spacing, turn after turn | Nominal pitch and how it is measured |
| Link thickness and height | Decides how the link sits on the tooth and on the drum bars | Both values, new condition |
| Rod diameter | The tooth pocket must suit the rod it picks up | Rod diameter and material |
| Edge type and weld finish | The inner edge rides on the drum; rough welds wear guides and bars | Edge type, weld finish requirement |
| Turn ratio and inside radius | Decide how far the links collapse on the curve | Turn ratio, inside radius, drum diameter |
| Running direction | Clockwise or counter-clockwise changes which side carries load | Direction, ascending or descending |
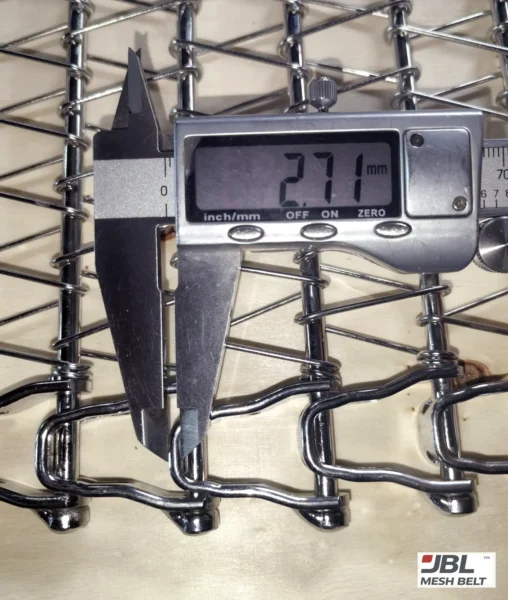
Two readings from our own projects show why “new condition” matters. On a waffle cooling spiral, the customer’s original link measured 2.42 mm after years of service; the new link was made at 2.71 mm. A drawing taken from a worn belt would have carried the wear into the new design. On a bakery cooling spiral in Melbourne, we read a 27.41 mm pitch and a 5.03 mm rod on the customer’s sample before matching the new belt and its sprockets.
Which sprocket details must be on the drawing before release?
I treat a sprocket as part of the drive system, not as a separate part. These are the fields I check on every sprocket drawing:
| Sprocket field | What goes wrong if it is missing |
|---|---|
| Belt or chain pitch it drives | Teeth meet the rods out of step; the belt rides up and jumps |
| Tooth profile and tooth count | Pitch diameter changes; engagement point moves |
| Outside diameter, pitch diameter, hub | Belt height and clearance change at the drive |
| Bore: round or square, size and fit | Sprocket cannot be fitted, or runs loose |
| Keyway width and depth — stated separately | The single most common incomplete field |
| Set screws, thickness, number of rows, split design | Assembly and maintenance problems |
| Material | Wear, marks on the belt, or cracking in the cold |
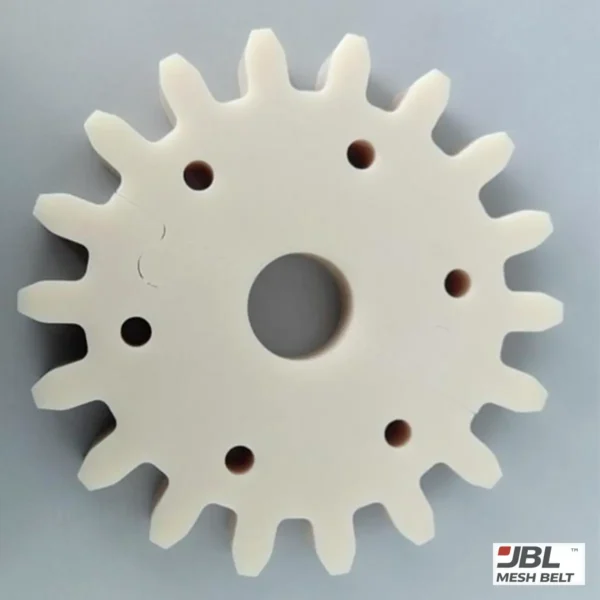
Two spiral examples from our sprocket records: a stainless steel sprocket with 16 teeth for a 38.1 mm link pitch on 6 mm rods, and a POM sprocket with 14 teeth for a 27.4 mm link pitch on 5 mm rods. The belts are different, so the sprockets are different — one drawing does not fit both.
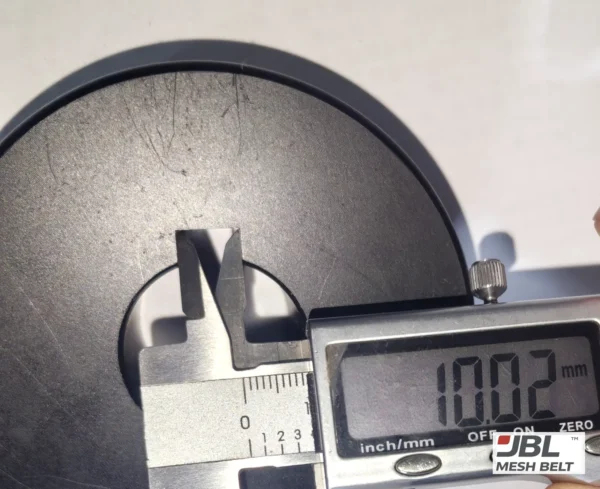
On the waffle spiral project, there was no drawing from the original builder. New sprockets were made to the customer’s originals — bore, keyway and tooth — and the keyway read 10.02 mm on the new part. That reading is on the record, so the next order is made to the same number.
Which sprocket material suits the temperature?
| Material | Where we typically use it | What to confirm |
|---|---|---|
| SUS304 / SUS316 | Spiral, flat wire and chain-driven belts | Tooth surface finish, so it does not leave dark marks |
| UHMWPE | Side-driven belts, Z-type ladder and eye link belts | Clean edges and bore, no excess burrs |
| Nylon | Bakery cooling spirals and similar | Temperature range and wear |
| POM | Selected spiral and side-driven projects | Ordinary POM is not suited to freezing. A low-temperature grade is chosen for the working temperature and confirmed in writing |
If your spiral runs below zero, put the working temperature on the sprocket drawing, not only on the belt drawing. It changes the material choice.
How is engagement checked before the design is released — and before shipment?
The checks that matter are the ones you can see.
- Turn ratio, drum diameter and sprockets first. On spiral, self-stacking and side-driven projects, I confirm these three before quotation. If one is unknown, the project stays in engineering review.
- A trial length against the original or the drawing. On the waffle spiral, a trial section was linked into the customer’s original belt and photographed side by side. The customer approved it from the photos before bulk.
- A turn test on a drum. On a spiral replacement in Malaysia, the trial run was turn-tested before bulk production.
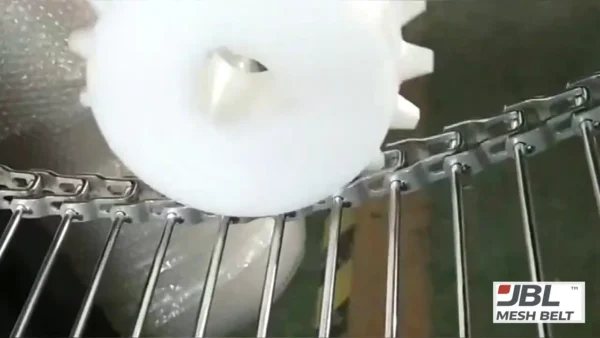
- A sprocket running test on the new belt, where sprockets are supplied. On the Melbourne and waffle projects, a sprocket was run on the new belt to check tooth engagement before the crates were closed.
One lesson from Melbourne is worth putting on any spiral drawing: the original belt had rough rod-end welds, and they scored the plastic guide strips along the belt path. Weld finish is an engagement and wear issue, not only a cosmetic one. On the new belt, the weld finish was specified and checked on the sample.
What should an OEM send for an engagement review?
- Belt drawing, or the belt specification: pitch, rod, link, edge, material
- Drum diameter, turn ratio, inside radius, running direction, tiers
- Drive arrangement: low-tension, direct, side or edge drive; location of drive and take-up
- Sprocket drawing, or tooth count, bore, keyway width and depth, material
- Working temperature range and cleaning method
- Photos of the drive area, if the machine already exists
You do not need everything to start. Send what you have, and I will list what is still missing before any quotation. Email info@jblmeshbelt.com or WhatsApp +86 138 1487 2506.
Spiral belt drive engagement: FAQ
Should the belt and sprockets come from the same supplier?
It is not required, but they should be designed and checked together. When one supplier makes both, the sprocket can be run on the new belt before shipment, and both readings are kept on one record.
Is matching the pitch enough for good engagement?
No. Tooth profile, tooth count, rod diameter, link thickness and the turn ratio on the drum all change where the belt meets the drive. Two belts with the same pitch can engage very differently.
Can sprockets be made without the original drawing?
Yes, from the customer’s original sprocket. Tooth, hub, bore, keyway and thickness are measured with a caliper, and the new sprocket is checked on the new belt. On the waffle spiral project, this is how the sprockets were remade.
What plastic sprocket should I use for a spiral freezer?
It depends on the working temperature. Ordinary POM is not suited to freezing; a low-temperature grade, UHMWPE or another material is chosen for your temperature and confirmed in writing before production.
How do price and lead time work?
They depend on size, material and quantity and are confirmed in writing in each quotation.